The mill certificate and heat number are matched to the grade on your drawing before bar reaches a machine, so each lot traces back to its melt.

Divine Precision
Get Instant Quote
Divine Precision
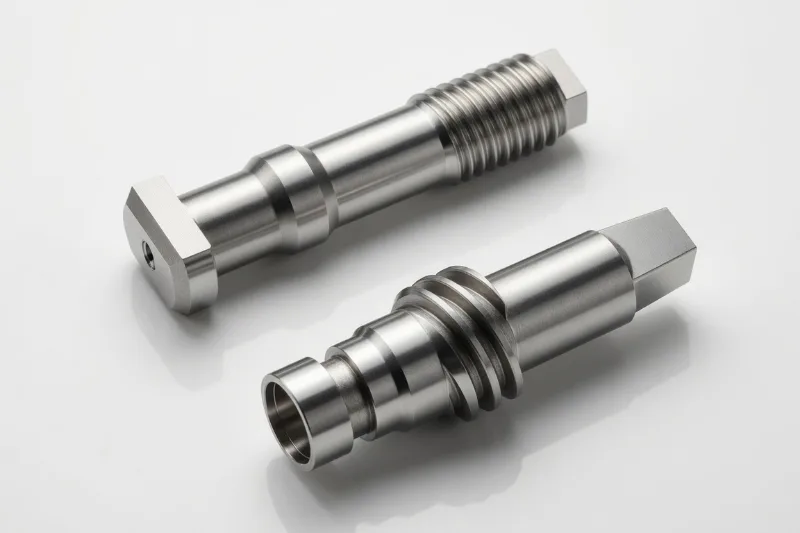
Shafts, pins, valve stems and fittings turned from bar to your drawing, passivated or electropolished. 17-4PH bearing diameters are ground to ±0.005 mm, with the condition set per drawing. Send your drawing for a quote.
| Dimensional capability | |
|---|---|
| Process | CNC turning from bar, ground tight diameters; slender small parts on swiss cnc machining |
| Diameter range | Bar Ø 3–65 mm; billet for larger sections |
| Length | Per drawing, L/D reviewed at quote; billet to 200 mm |
| Diameter tolerance | Ground ±0.005 mm, turned ±0.01 mm |
| Surface finish | Ra 1.6 µm standard; Ra 0.4 µm when called out |
| Threads | M1.6–M36, UNC / UNF |
| Secondary features | Cross holes, flats, knurls, grooves, laser marking |
| Ordering | |
|---|---|
| Basis | Build-to-print; other metals under CNC turned parts |
| Minimum order | 1 piece |
| Prototype lead time | 3 days (fast); 2–3 weeks typical |
| Production lead time | 4–6 weeks typical |
| Batch size | 100–100,000+ pieces |
| File formats | STEP or IGES with 2D GD&T drawing; SLDPRT, PRT, DWG, PDF |
| Packing | VCI film, anti-rust oil, trays; packing machined parts for sea freight |
303 vs 304 stainless steel comes first; passivation of stainless steel follows.
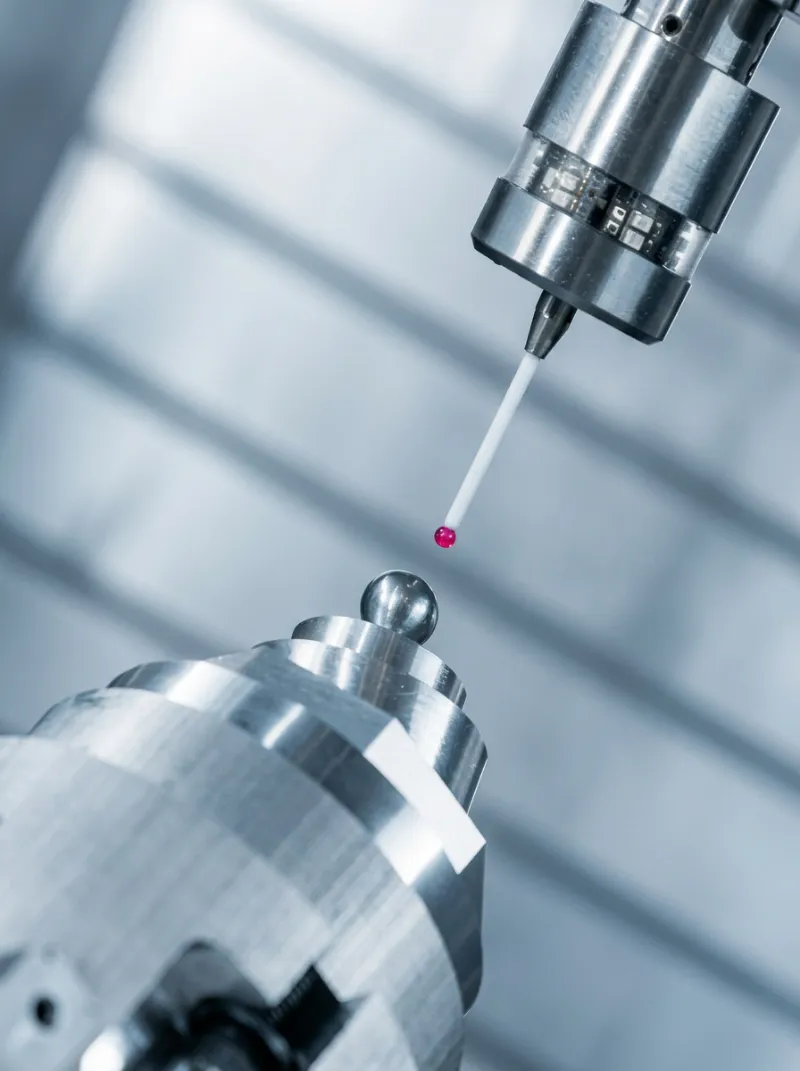
The mill certificate and heat number are matched to the grade on your drawing before bar reaches a machine, so each lot traces back to its melt.
The first piece is measured on the CMM and the FAI report is sent to you. The run begins only after your sign-off.
Operators sample critical dimensions through the run to an AQL plan, so drift is corrected at the machine instead of at the end.
Every lot gets a 100% dimensional and visual check. The material certificate and inspection record ship standard; PPAP packages are available on request. See the precision machined medical parts case, made under the ISO 9001 quality system with full traceability.
303 pins and 304 shafts with heat-number traceability; PPAP packages on request.
17-4PH drive shafts and pins, ground to ±0.005 mm on bearing diameters.
316L valve stems and fitting bodies from bar to Ø 65 mm; flat covers via Laser Cutting and its thickness guide.
304 pins and small fasteners, bead-blasted or polished, Ra 0.4 µm when called out.
Passivated 316L connector pins and fittings for moisture-exposed equipment.
303 pins and fasteners from Ø 3 mm, with laser-marked serial or Data Matrix codes.
Still looking for something? Contact us and our team answers within one business day.
Ask a QuestionStainless turns well on a rigid setup, and 304 generally cuts more easily than 316L. Choose 316L when chlorides or chemicals are the concern. If corrosion demands are modest, 303 is the easiest of the three, at some cost in corrosion resistance and weldability.
Call out the condition on the drawing, for example H900 or H1150, plus the hardness range you need. Lower H numbers give higher strength; higher ones trade strength for toughness. We work to the condition per your drawing.
Aging shifts dimensions slightly, so tight diameters are best finished after it, typically by grinding, with roughing done earlier. State your preference on the drawing; the route is confirmed on the quote.
Ground diameters hold ±0.005 mm and turned diameters ±0.01 mm. Ra 1.6 µm is the standard finish, and Ra 0.4 µm is available when called out. Mark critical features on the drawing so they are checked first.
One piece is the minimum. Prototypes ship in 3 days on the fast route, with scope confirmed at quote, or in 2–3 weeks typically. Production lots run 4–6 weeks typically. Rush options exist for many jobs and are confirmed per quote.
A material certificate showing mill and heat number ships with every lot, with the inspection record from the 100% final check. An FAI report is sent before production starts. PPAP packages are available on request.
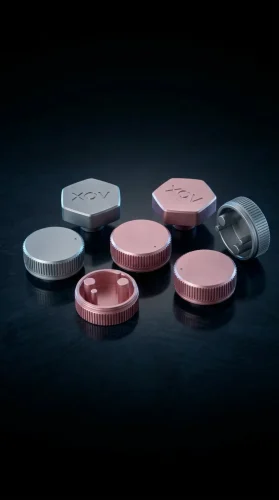
One Gr.5 prototype, heat-traced, quoted within one business day. Titanium CNC machining in Gr.2 and Gr.5, plus Inconel machining in high-nickel alloys, made to your drawing.
Made-to-print turned parts and precision turned components from our Hong Kong and Dongguan facilities, one piece to 100k+ per run, in aluminium, stainless steel, brass and steel.
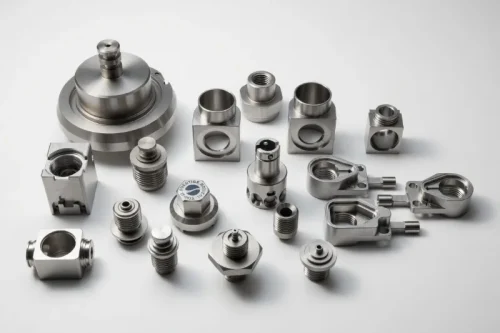
Machined contacts for connectors and sensors, Swiss-turned in volume, with the mating diameter ground to ±0.005 mm. Send your drawing and the first pieces can ship in 3 days.
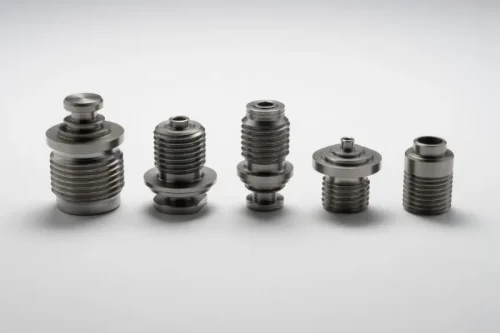
Custom hydraulic fittings, adapters, plugs and valve bodies machined to your drawing, from one piece. Send your drawing and get a reply within one business day.
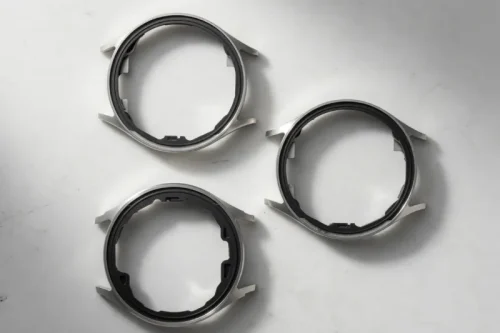
Made-to-print port housings and rings for pressure, transducer and oxygen sensors, with sealing faces to Ra 0.4 µm on request and threads and O-ring grooves cut to your drawing.
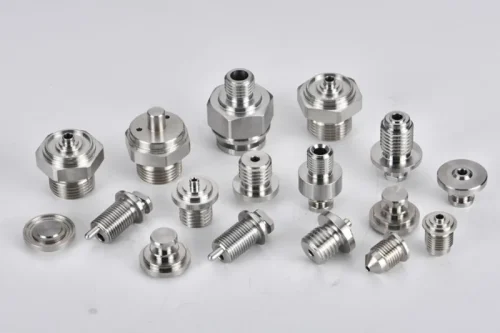
Made-to-print VCR-type fittings: glands, nuts and gaskets, electropolished and packed particle-free.
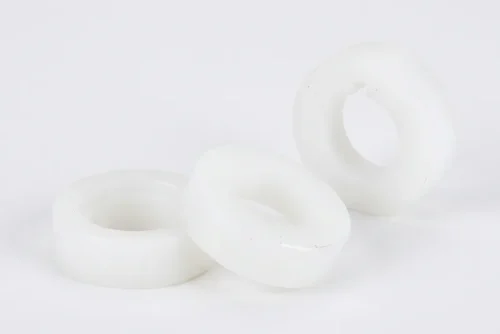
Rings, spacers, insulators and wear parts machined burr-free from PEEK, POM, PA66 and PTFE. Upload your drawing and get a quote within one business day.
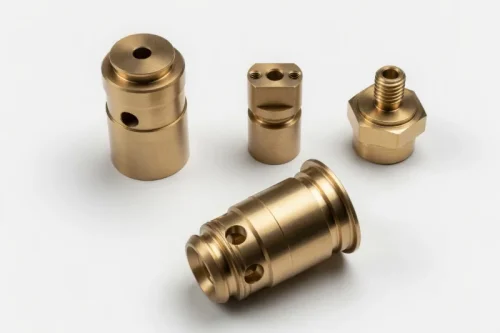
Nozzles, hex fittings, inserts and connector bodies machined in free-machining brass, plated on request.
Send your CAD drawings, 2D/3D files, or technical documents securely. Our team reviews promptly, protects your IP fully — and signs an NDA on request.